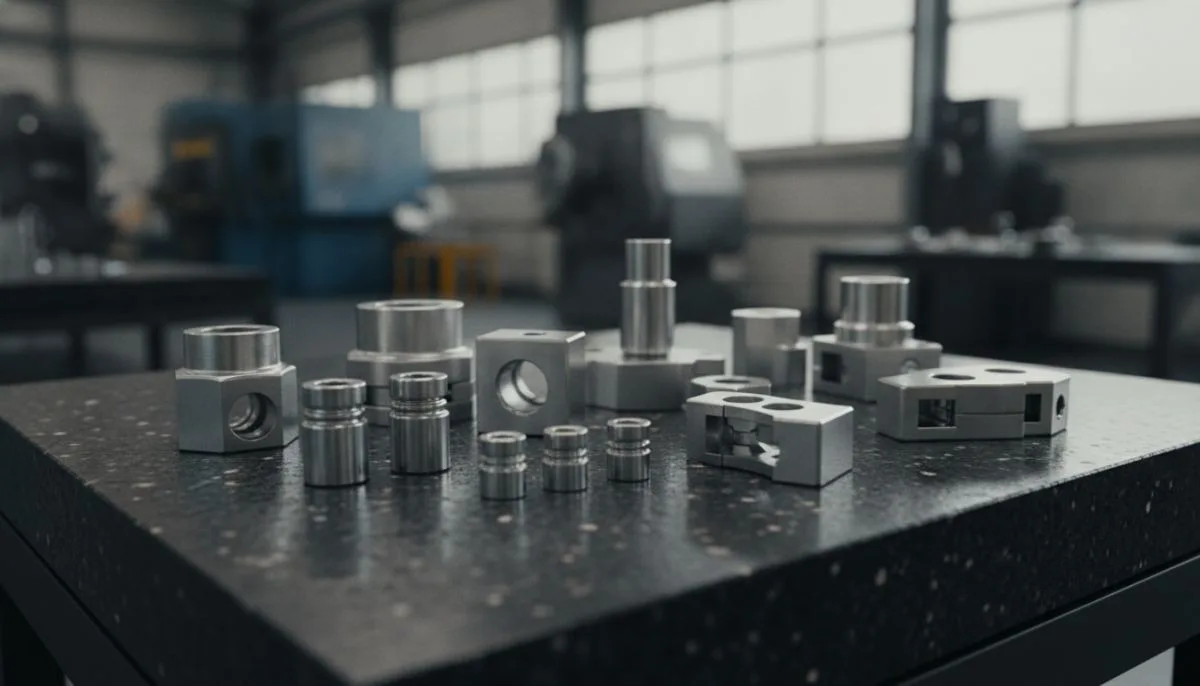
CNC Swiss Machining Deburring and Edge Cleaning Guide
Comprehensive guide on CNC Swiss lathe deburring techniques, edge finishing, surface quality, and dimensional tolerance control for precision lock parts.
In the field of precision subtractive machining, tight tolerances, immaculate surface finishes, and high-speed repeatability define success. Among the essential stages of component manufacturing, thorough deburring in CNC automatic and Swiss lathe machining directly impacts both mechanical assembly reliability and the operational lifespan of the end mechanism. Whenever rotary or axial cutting inserts shear metal stock on lathe beds or Swiss-type sliding headstock machines, plastic deformation occurs at the exit edges of the cutting path. This deformation leaves behind minute, jagged metallic projections commonly known as burrs. When dealing with intricate components such as lock cylinder plugs, shafts, pin chambers, and hydraulic fittings, leaving micro-burrs intact invariably leads to mechanical jamming, accelerated friction wear, or premature functional failure.
Modern mass production lines require thousands of batch-turned parts to conform to consistent dimensional standards. Whether handling contract machining projects or dedicated cylinder lock assemblies, an imperceptible edge protrusion exceeding specification can disrupt an entire locking mechanism. Consequently, deburring operations performed after primary machining are never mere secondary cleaning steps; they serve as an integral parameter of comprehensive quality assurance, assembly verification, and extended mechanical endurance.
Root Causes of Burr Formation in CNC Swiss Machining
Burr creation is an inherent physical byproduct of the metal cutting mechanics involved in turning, milling, and drilling. However, when edge buildup exceeds manageable thresholds, the issue typically stems from worn tool geometries, sub-optimal cutting feeds and speeds, or inconsistencies across the raw material microstructure. As a cutting tool enters and ultimately exits the workpiece edge, cutting forces exceed the yield strength of the metal. Instead of shearing cleanly off as a standard chip, the remaining marginal metal rolls and bends along the exit margin, forming a resilient burr.
Incorrect selection of spindle speed and feed rate exacerbates burr thickness and height. Excessively elevated feed rates generate extreme thermal concentration along the cutting edge, leading to localized metal smearing. Conversely, excessively light feeds can cause the tool nose radius to rub and burnish rather than shear the stock, severely destabilizing micron-level edge accuracy. Contract manufacturing workshops that experience inconsistent machine setups often observe fluctuating burr profiles across single production runs. For facilities managing high-mix contract turning, reviewing systematic guidelines such as part inspection criteria in contract CNC machining is vital for establishing reliable quality baselines.
Insufficient coolant concentration, inadequate delivery pressure, or poor nozzle aim also accelerate burr growth. When hot chips are not flushed away from the instantaneous shear zone, chips frequently weld onto the tool rake face, forming a built-up edge (BUE). Once a cutting insert develops a built-up edge, clean slicing gives way to tearing, leaving severe root burrs along deep chamfers, undercuts, and counterbores.
Mechanical and Chemical Deburring Methods for Turned Parts
Depending on batch volume, part geometry, parent metal characteristics, and specified finish allowances, manufacturing engineers utilize several targeted deburring techniques. For small, high-volume turned parts produced from free-cutting brass, stainless steel, or case-hardening carbon steel, vibratory tumbling stands as the industry standard mechanical solution. Workpieces are loaded into vibratory bowls filled with ceramic or synthetic abrasive media suspended in specialized chemical compounds and water. The harmonic oscillatory action causes continuous rubbing against external part profiles, naturally breaking off fine burrs while generating uniform, radiused edges.
When dealing with complex interior intersections, intersecting cross-holes, and blind galleries, advanced methods like thermal deburring (TEM) or high-pressure waterjet cleaning become indispensable. In thermal deburring, parts are sealed inside an airtight combustion chamber filled with a pressurized mixture of fuel gas and oxygen. A brief spark initiates a microsecond controlled deflagration; the momentary heat wave incinerates thin, high-surface-area burrs entirely without affecting the bulk structural integrity of the workpiece. This non-mechanical solution proves invaluable for precision lock components where miniature cross-drilled internal ports cannot be accessed by manual deburring brushes or mechanical rotary files.
Chemical and electrochemical deburring (ECD) methods utilize electrolytic dissolution to strip burrs from metallic edges. By directing electrical current through tailored electrolytes toward conductive edges, metal ions dissolve preferentially at sharp peaks. This yields a clean, bright edge finish while leaving overall body dimensions within defined print limits, provided cycle times are calculated accurately. To better understand how microscopic edge processing intersects with overall part stability, examining technical data on mass production tolerances in CNC automatic lathes provides essential operational context.
Significance of Edge Preparation in Locking and Security Hardware
Lock assemblies rely on the synchronized interaction of close-tolerance pins, springs, retainers, and turned housing shells. Even a single lingering micro-burr inside a cylinder plug channel can obstruct key insertion, hinder tumbler movement, or prevent pins from seating flush against their shear lines. In high-traffic building entrance solutions where components endure rigorous cyclic actuation, internal mechanical surfaces must remain flawless. Hardware designed for demanding security applications, such as heavy-duty electric rim cylinder with tube assemblies, depends completely on pristine pin chambers to prevent mechanical binding over years of daily usage.
Unremoved burrs pose more than just immediate assembly friction; microscopic fragments that fracture during operation can migrate into the internal plug shear line, leading to catastrophic cylinder lockup. The exact same vulnerability applies to window hardware, pivot studs, and sash locking accessories. Mechanical security hardware, such as a dependable PVC window safety device, requires precision-deburred pins and anchor studs so that latching movements remain fluid without galling metal surfaces.
Furthermore, when metal shaping involves sequential operations such as forging followed by precision secondary turning, residual stresses and localized grain flows alter edge burr characteristics. The orientation of the deformed metal grain influences burr tenacity during machining. Facilities integrating multiple manufacturing techniques like cold forging press stamping alongside precision turning must implement structured edge cleaning protocols tailored to the material condition.
Common Operational Pitfalls During Deburring Processes
Because deburring is frequently viewed as a final finishing step rather than a primary machining discipline, production lines frequently encounter procedural errors that risk out-of-spec dimensions or scrap generation:
- Excessive Vibratory Cycle Times: Running parts in vibratory bowls far past the required deburring interval causes over-radiused corners, thread distortion, and the loss of critical bearing seat diameters.
- Incorrect Abrasive Media Sizing: Choosing media geometries that match the size of cross-holes or bores leads to wedging, trapping abrasive stones inside precision channels where they are difficult to extract.
- Inadequate Rinsing and Drying: Leaving abrasive compound residues or slurry films on turned components causes rapid oxidation, surface staining, and galvanic corrosion during subsequent storage.
- Neglecting Upstream Tool Wear: Attempting to compensate for excessively worn lathe turning inserts solely by extending secondary deburring routines drives up finishing costs and damages dimensional yields.
Frequently Asked Questions
Can burr formation be eliminated entirely during CNC turning?
Due to the plastic deformation mechanics of metals under shear stress, complete burr prevention is rarely possible on standard tooling exits. However, using optimized cutting speeds, high-pressure through-tool coolant, balanced edge prep geometries, and integrated in-cycle back-chamfering cycles minimizes burr volume to negligible levels, dramatically reducing secondary finishing times.
Do brass and stainless steel parts require identical deburring protocols?
No. Free-cutting brass forms brittle, easily detached chips and burrs, allowing fast deburring with synthetic plastic media and mild compounds. In contrast, stainless steel is ductile and work-hardens readily, demanding denser ceramic media, aggressive abrasive compounds, and higher mechanical energy inputs to shear tough edge projections.
Can vibratory finishing adequately clean small internal cross-drilled holes?
Vibratory media cannot clean internal bores if the media stone dimensions exceed hole diameters. Attempting to force small stones into narrow orifices often leads to stone lodge-in. Internal burrs in small ports are far more reliably cleared using automated brushing, thermal deburring, or high-pressure fluid jets.
Does deburring alter critical external dimensions on turned workpieces?
When process parameters, media density, and cycle durations are controlled, deburring targets only high-energy sharp edges and projections. However, aggressive mechanical cycles or uncontrolled chemical etching can remove base metal from flat planes and outside diameters, risking tolerance violations.
Deburring Control and Continuous Improvement in Machining Workshops
Managing burrs cost-effectively requires a holistic manufacturing mindset rather than isolated troubleshooting. Improvement begins during CNC programming and CAM toolpath design. Programmers should incorporate secondary chamfer passes, helical deburring paths, and edge-break routines into primary lathe cycles whenever cycle time permits. Concurrently, machine operators must track insert wear trends, replacing worn tooling before dull cutting edges push burr heights past accepted operational standards.
Post-machining finishing departments should establish standardized recipes matching part geometry and alloy composition. Media wear rates, fluid detergent concentrations, bath pH levels, and rinse stages must be logged consistently to maintain repeatable part yields. To discuss contract manufacturing projects, establish reliable component quality, or evaluate custom security hardware solutions, please contact us.
You May Also Like Kopyala